Choosing TIG Filler Rods
Choosing a TIG filler rod becomes easier when you start with the job in front of you. Joining mild-steel tube, repairing an aluminium casting and fabricating stainless equipment each place different demands on the weld. Once you know which metals you are joining and what the finished part needs to withstand, the codes on the packet become much more useful. This guide explains the common filler types, where they are usually used and the differences that can influence your choice.
There are two decisions to work through: the filler alloy first, then the rod diameter. The alloy determines what you are adding to the joint, while the diameter affects how you feed it into the weld pool. The tables below help you compare the common options. Where the job has a welding procedure, use its requirements to make the final selection, alongside the filler manufacturer’s data sheet.
Browse the full range of TIG filler rods, or use the material guide below to find the relevant section.
In this guide:
Understanding AWS TIG Filler Rod Codes
On a packet of steel TIG rods, you might see AWS A5.18 alongside a code such as ER70S-6. These describe two different things. AWS A5.18 is the American Welding Society specification covering that family of carbon-steel fillers, while ER70S-6 identifies a particular grade within it. Reading the grade code helps you understand what the rod contains and the properties it is classified to provide.
How to Read ER70S-6
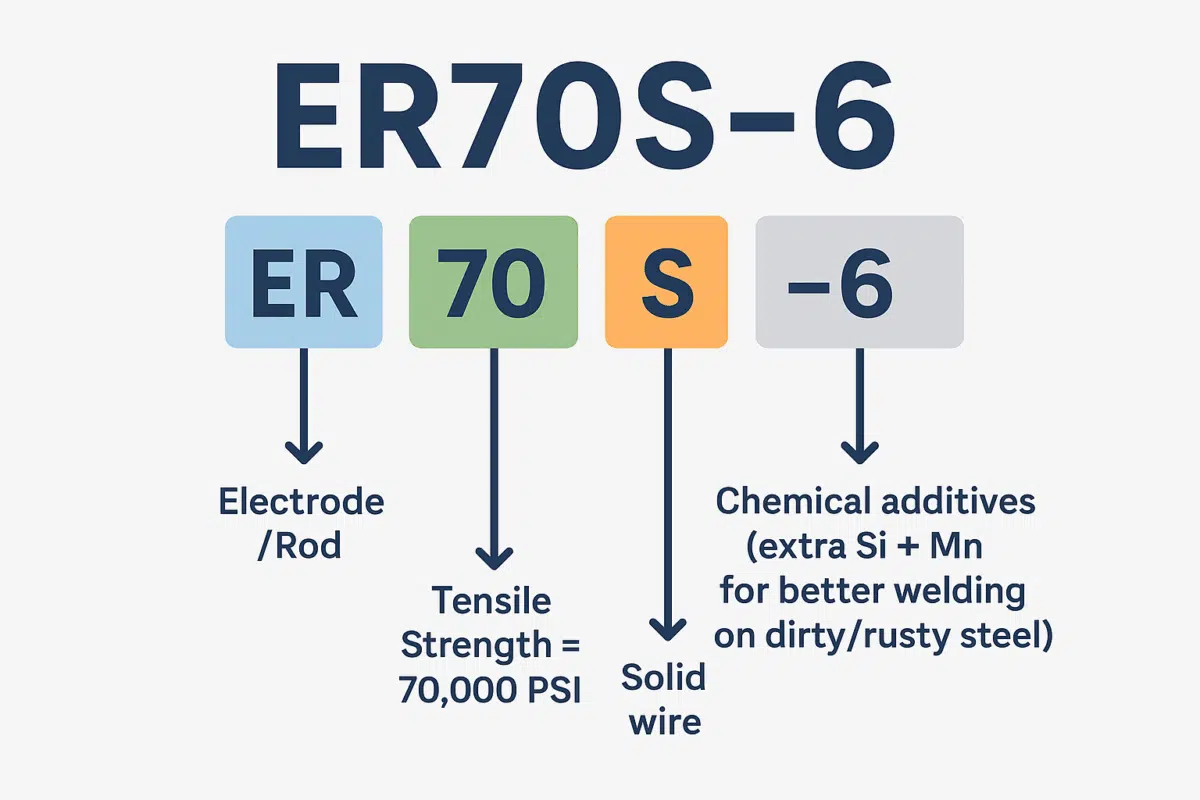
| Part of the code | How to read it |
|---|---|
| ER | Electrode or rod. The alloy can be supplied as current-carrying wire for MIG/MAG or as filler fed separately into the pool for TIG. |
| 70 | The minimum weld-metal tensile strength under the classification test conditions: 70,000 psi, or about 480 MPa. The strength of your finished joint also depends on how it is made. |
| S | Solid wire or rod. |
| -6 | Identifies the chemical composition, including manganese and silicon deoxidisers. It is a grade number rather than a percentage or quality score. |
Once you understand ER70S-6, it is tempting to read every filler code the same way, but the meaning changes between material families. In ER308L, for example, 308 identifies a stainless composition and L means low carbon. In ER4043, the number identifies an aluminium alloy. Neither uses the number to state tensile strength in the way ER70S-6 does.
Most rods used for everyday TIG work are solid, although specialist cored products are also available. You may also find the same ER classification on both TIG rods and MIG wire, because the alloy can be supplied for either process. When ordering, choose the form and diameter intended for your equipment, then follow the product’s guidance on shielding gas and welding conditions.
UK Trade Names and BS Designations
If you buy consumables from a UK welding supplier, you will often encounter older British designations such as A15 and A18. These remain useful names to recognise: A15 is commonly used for ER70S-2, and A18 for ER70S-6. The same pattern appears in low-alloy fillers, with A31, A32 and A33 commonly used for ER80S-D2, ER80S-B2 and ER90S-B3 respectively.
The shorthand becomes less reliable when different naming systems are treated as exact equivalents. A17, for instance, describes a low-silicon steel filler and should not automatically be translated as ER70S-3. A name such as 307Si can also refer to a modified stainless composition. The full classification on the data sheet is the useful reference when comparing products from different suppliers.
Quick Guide: TIG Rods by Material
Start with the material you are working on and use the middle column to recognise the filler codes you are likely to encounter. The sections that follow explain how to choose between them, including the exceptions that matter for particular alloys and service conditions. Each range link takes you to the relevant products, where you can see the available grades and sizes.
| Material or job | Common filler examples | Shop the range |
|---|---|---|
| Mild / carbon steel | ER70S-2, ER70S-3, ER70S-6 | Mild steel TIG rods |
| High-strength and low-alloy steel | ER70S-A1, ER80S-D2, ER80S-B2, ER90S-B3, ER100S-G, ER110S-G | High-strength steel TIG rods |
| Stainless steel | ER308L, ER316L, ER310, ER347 | Stainless steel TIG rods |
| Dissimilar steels | ER309L, ER309LSi, ER312; selected 307-type products | Stainless fillers for dissimilar joints |
| Duplex and superduplex stainless | ER2209, ER2594 | Duplex stainless TIG rods |
| Aluminium | ER1070, ER4043, ER4047, ER5356, ER5183, ER5556 | Aluminium TIG rods |
| Magnesium | ERAZ61A, ERAZ92A and specialist alloy-specific fillers | Magnesium TIG rods |
| Titanium | ERTi-1, ERTi-2, ERTi-5, ERTi-7, ERTi-23 | Titanium TIG rods |
| Nickel alloys and cast-iron repair | ERNiCr-3, ERNiCrMo-3, ERNiCrMo-4, ERNiCu-7; purpose-made bare cast-iron fillers | Specialty alloy TIG rods |
| Copper, bronze and TIG brazing | ERCu, ERCuSi-A, ERCuSn-C, ERCuAl-A2 | Copper and bronze fillers |
| Hardfacing and tooling repair | Product-specific iron-, nickel- or cobalt-based surfacing alloys | Hardfacing rods |
You will notice that the table groups rods by material rather than sheet thickness. The same filler alloy can be supplied in several diameters and used on a wide range of joints. Thickness becomes important when you choose the rod size, current, joint preparation and number of passes, once you have established which alloy the weld needs.
Mild Steel TIG Filler Rods (AWS A5.18)
For everyday mild-steel fabrication, ER70S-2 and ER70S-6 are two grades you will often come across. Both contain deoxidising elements, which help control oxygen in the weld pool and reduce the risk of porosity, but they use different combinations of those elements. Either may suit an ordinary fabrication job, depending on the weld properties required; the table below explains where each tends to fit.
Browse mild steel TIG rods.
| Filler | Common UK name | Where it fits |
|---|---|---|
| ER70S-2 | A15 | Widely used for mild-steel TIG work, including tube joints and pipe roots. Aluminium, titanium and zirconium provide the additional deoxidisers. |
| ER70S-3 | Use the product’s declared designation | A general fabrication option for well-prepared carbon steel. Its AWS classification should be compared directly when choosing an equivalent product. |
| ER70S-6 | A18 | A common fabrication filler with higher manganese and silicon to help deoxidation and flow. Joint cleaning remains part of the preparation. |
| A17 | A17 | A low-silicon UK filler designation used for some work that will be enamelled or galvanised. Its composition and current classification come from the particular product’s data sheet. |
Whichever grade you choose, start with clean metal. Removing rust, paint, oil and mill scale gives the filler a sound joint to work with, and its deoxidisers are not a reason to skip that preparation. If a welding procedure names a grade, use it. You may also see ER70S-A1 alongside these rods, but its molybdenum content puts it in the low-alloy group covered next.
High-Strength and Low-Alloy Steel TIG Rods (AWS A5.28)
With higher-strength and low-alloy steels, it helps to ask what the alloy is expected to do in service. A structural part may need a stronger weld, equipment working in the cold may need better impact toughness, and hot pipework may need to retain its properties at elevated temperatures. Those are different requirements, which is why choosing the largest strength number on the packet is not enough.
Browse high-strength and low-alloy steel TIG rods.
| AWS classification | Common name or alloy family | Where it fits |
|---|---|---|
| ER70S-A1 | 0.5% molybdenum steel | Carbon-molybdenum pipework and pressure equipment requiring this filler. It belongs to AWS A5.28 even though its strength prefix begins ER70. |
| ER80S-D2 | A31; manganese-molybdenum | Certain higher-strength carbon and low-alloy steels, with the choice guided by toughness and any heat treatment as well as strength. |
| ER80S-B2 | A32; approximately 1.25% chromium / 0.5% molybdenum | Matching chromium-molybdenum steels such as P11 pipe, used with the appropriate preheat and heat-treatment procedure. |
| ER90S-B3 | A33; approximately 2.25% chromium / 1% molybdenum | Matching chromium-molybdenum steels such as P22 pipe, where the required properties depend on the welding and heat-treatment conditions. |
| ER80S-B6 | Approximately 5% chromium / 0.5% molybdenum | Matching 5Cr-0.5Mo refinery and process-equipment steels under their welding procedure. |
| ER80S-Ni1 / ER80S-Ni2 | Nickel-alloyed steel fillers | Applications requiring low-temperature impact toughness. The product’s impact-test results show the temperatures and performance it supports. |
| ER80S-G | Composition varies by product | Specialist low-alloy applications, including weathering steel for products made for that purpose. The G suffix alone does not identify the application. |
| ER100S-G / ER110S-G | Higher-strength compositions that vary by product | Equipment and structural joints requiring these strength classes, with toughness and cracking risk considered alongside the strength match. |
For chromium-molybdenum pipework, the filler and heat treatment need to be considered together. The intended weld properties depend on the preheat, temperature between passes and any treatment after welding, so the procedure should guide all of those choices.
Weathering steel raises a different question: how the weld will resist atmospheric corrosion. Some ER80S-G products are formulated for that purpose, but others are designed for different low-alloy applications. Look for a product intended for the particular weathering steel, and treat colour matching as a separate consideration rather than something the G suffix guarantees.
Stainless Steel TIG Filler Rods (AWS A5.9)
For familiar stainless grades, the filler choice often starts with a straightforward pairing: ER308L for 304 or 304L, and ER316L for 316 or 316L. From there, consider what the part will be exposed to, whether that is food-processing conditions, chemicals, seawater or heat. The L suffix means low carbon, which helps reduce chromium-carbide formation during welding and the associated risk of corrosion.
Browse stainless steel TIG rods.
| AWS classification | Common uses | What helps you choose |
|---|---|---|
| ER308L | 304 and 304L stainless fabrication. | The familiar starting point for these grades, with service conditions guiding the final selection. |
| ER316L | 316 and 316L stainless in chemical, marine and process equipment. | Its molybdenum improves resistance to some forms of corrosion compared with 308L. Suitability still depends on the environment, particularly where chlorides are present. |
| ER309L / ER309LSi | Many stainless-to-carbon-steel joints and some overlays. | Extra alloy content helps accommodate the carbon steel mixed into the pool. The Si version generally improves how the weld spreads and wets the joint. |
| ER310 | Matching 310-type stainless and certain high-temperature components. | Chosen for the particular heat-resistant alloy and its operating conditions. |
| ER347 / ER347Si | 321 and 347 stainless applications requiring these fillers. | Niobium-stabilised compositions used where their properties suit the service. High-temperature requirements and any silicon limit influence the choice. |
Once the filler is chosen, preparation and shielding help preserve the corrosion resistance you are aiming for. An exposed root may need a gas purge or another backing arrangement to protect its underside from oxidation. Clean tools reserved for stainless and any required heat-tint removal are part of that process too. Severe root oxidation, often called sugaring, needs attention to the welding conditions; changing to a more highly alloyed rod will not correct it.
TIG Filler Rods for Dissimilar Steels
Joining stainless to mild steel introduces an extra consideration: some of each parent metal melts into the pool along with the filler. That mixing is called dilution, and it changes the composition of the finished weld. ER309L is commonly chosen for these joints because its extra alloy content helps accommodate the carbon steel. The particular stainless grade and service temperature may lead to another choice, including a nickel filler.
You will find ER309L, ER309LSi, ER312 and 307-type repair products within the stainless steel TIG rod range. The useful distinction is what each is designed to contribute to the joint, rather than how easily it produces a tidy bead.
| Filler | Common uses | What helps you choose |
|---|---|---|
| ER309L | Many austenitic-stainless-to-mild-steel joints and stainless overlays. | A common starting point, with the particular stainless grade and service temperature determining suitability. |
| ER309LSi | Similar joints where improved wetting is useful. | Higher silicon can help the bead spread more smoothly, while the same alloy-compatibility and service considerations still apply. |
| ER312 | Certain difficult repairs and dissimilar-steel joints. | Its high-ferrite deposit resists weld-metal cracking. The parent steel still needs to be identified and assessed for welding. |
| 307-type / 307Si products | Some manganese-steel joints, dissimilar repairs and buffer layers under hardfacing. | Application guidance is product-specific; the declared classification may describe a modified composition. |
Repair work can be less straightforward when the parent metal is unknown. ER312 is often associated with difficult repairs because its deposit resists cracking, but the surrounding steel can still harden or crack during welding. Identifying the component material is therefore an essential first step, particularly on load-bearing, hardened or fatigue-loaded parts, before deciding on the filler and heat treatment.
Duplex Stainless Steel TIG Rods (AWS A5.9)
Duplex stainless needs a little more explanation because its properties depend on the balance between two structures in the metal: ferrite and austenite. Welding changes that balance as the joint heats and cools. Duplex fillers are designed to help the weld develop the required structure, often by containing more nickel than the parent steel, so the filler composition may deliberately differ from the material being joined.
Browse duplex stainless TIG rods.
| AWS classification | Common uses | Choosing the product |
|---|---|---|
| ER2209 | 2205 duplex stainless and other approved combinations. | A common choice for 2205, selected alongside the corrosion requirements and welding procedure. |
| ER2594 | 25% chromium superduplex grades requiring this filler. | The parent grade and its alloying additions determine whether this is the appropriate superduplex filler. |
That is also why temperature control matters throughout a duplex weld. Rapid cooling can leave too much ferrite, while excessive heat or too long at temperature can allow brittle phases to form. The aim is to stay within a suitable working range, following the qualified procedure for heat input, temperature between passes, shielding gas and filler addition. Simply reducing the current or leaving out filler on a tight joint can upset the balance you are trying to achieve.
Aluminium TIG Filler Rods (AWS A5.10)
With aluminium, finding the parent alloy number is the first useful step, because it helps narrow down which fillers are suitable. You will often come across ER4043 and ER5356, and some jobs allow either. Where both are suitable, the choice comes down to what you need from the finished weld: 4043 is often valued for its flow and resistance to cracking, while 5356 may be preferred for its fillet-weld strength or closer colour match after anodising. Knowing how the part will be used and finished helps you decide which of those qualities matters most.
Browse aluminium TIG rods.
| AWS classification | Alloy family | Where it fits |
|---|---|---|
| ER1070 | High-purity aluminium | Compatible commercially pure aluminium where purity or conductivity is important. Other pure-aluminium designations need their own compatibility check. |
| ER4043 / ER4043A | Approximately 5% silicon | Many 6xxx alloys, including 6061 and 6063, and compatible castings. Often chosen for flow and resistance to cracking, with anodised colour a consideration. |
| ER4047 | Approximately 12% silicon | Selected aluminium-silicon castings and jobs benefiting from a highly fluid filler. The casting alloy and joint fit still determine suitability. |
| ER5356 | Approximately 5% magnesium | Many 5xxx alloys and selected 6xxx jobs, particularly where fillet-weld strength, ductility or anodised colour matter. Sustained service temperature can limit its use. |
| ER5183 | Magnesium-manganese alloy | High-strength joints in compatible alloys such as 5083, including marine fabrication, where its as-welded properties meet the job’s requirements. |
| ER5556 | Magnesium-manganese alloy | Selected 5xxx structural alloys where a higher-strength weld deposit is required, subject to alloy compatibility and service conditions. |
Before settling on a filler, look at the limits associated with the parent alloy and service temperature. ER4043 should not be used on 5xxx alloys containing more than about 2.5% magnesium. ER5356 and other high-magnesium fillers also need particular care where the component will remain above about 65°C for long periods, because their corrosion performance can deteriorate. The alloy manufacturer’s selection chart helps you work through these limits alongside the strength, ductility and finish you need.
It is worth considering the effect of welding on the parent metal as well as the filler. Heat-treated aluminium such as 6061-T6 can soften around the weld, and choosing a stronger rod does not restore the original properties throughout that area.
When it comes to preparation, remove oil and grease before tackling the oxide layer with a dedicated stainless-steel brush or another approved method. Keeping both the joint and the filler clean gives you a better starting point for a sound weld.
Magnesium TIG Filler Rods (AWS A5.19)
On a magnesium repair, the casting or material designation is especially useful because it tells you which alloy family you are dealing with. An AZ-series magnesium-aluminium-zinc casting can need a different filler from a rare-earth magnesium casting, even when the parts look similar. Once you have identified the alloy and its condition, you can use the repair instructions and filler data to narrow the choice.
Browse magnesium TIG rods.
| Filler designation | Where it is commonly used | How to narrow the choice |
|---|---|---|
| ERAZ61A | Compatible magnesium-aluminium-zinc alloys, including certain wrought products. | Use the parent alloy designation and required weld properties to compare the manufacturer’s recommendations. |
| ERAZ92A | Selected AZ-series magnesium castings. | The casting grade and repair instructions establish whether it is the appropriate AZ filler. |
| AZ101A | Specialist repairs to certain magnesium-aluminium-zinc castings. | Compare the product’s declared specification and application list; naming conventions vary. |
| EZ33A and other specialist grades | Certain rare-earth magnesium alloys. | Selection depends on the exact alloy, its heat-treatment condition and the approved repair method. |
Preparation needs the same attention as filler selection, with contamination and oxidation removed by a method suitable for the alloy. Plan for the debris that preparation produces too: magnesium dust and swarf present a serious fire risk and must be kept away from the welding area. Have the appropriate metal-fire arrangements in place before starting, and never use water on a magnesium fire.
Titanium TIG Filler Rods (AWS A5.16)
A matching titanium filler grade is often the starting point, but the final choice involves a balance between strength, ductility and corrosion resistance. Some procedures deliberately use a lower-strength filler to give the weld more ductility. This explains why a familiar rod such as ERTi-2 can be right for one job and unsuitable for another, particularly when you move from commercially pure titanium to a stronger alloy.
Browse titanium TIG rods.
| AWS classification | Alloy type | Where it fits |
|---|---|---|
| ERTi-1 | Commercially pure titanium | Applications calling for a relatively ductile, lower-strength titanium deposit. |
| ERTi-2 | Commercially pure titanium | Grade 2 fabrication and other joints whose procedure calls for this filler. |
| ERTi-5 | Ti-6Al-4V | Grade 5 alloy components in aerospace, industrial and other work needing the appropriate high-strength deposit. |
| ERTi-7 | Commercially pure titanium with palladium | Matching Grade 7 and other approved applications needing its corrosion-resistant properties. |
| ERTi-23 | Ti-6Al-4V ELI | Work requiring the extra-low-interstitial version of the alloy, with tighter control of oxygen and other elements to improve toughness. |
With titanium, choosing the rod is only one part of keeping the weld sound. The hot metal can absorb gases from the air and become brittle even after it has solidified, so protection needs to extend beyond the molten pool. A trailing shield protects the cooling weld, while a back purge protects the underside; some work is done inside an inert-gas enclosure instead. The filler, joint and tools also need to stay clean throughout the operation.
As you weld, the surface colour gives you a useful indication of how well that protection is working. Silver or light straw may be acceptable under the job’s specification, while blue, grey or white calls for an assessment of shielding and contamination. Colour is only part of that assessment, however: even a silver surface can conceal a problem. Use the inspection requirements to decide whether a weld can be accepted or needs further work.
Nickel Alloy TIG Filler Rods (AWS A5.14)
Nickel fillers are often encountered on jobs where corrosion or high temperature places demanding requirements on the weld. They also provide options for some dissimilar-metal joints. The familiar names can be a useful starting point, but Inconel, Monel and Hastelloy each cover alloy families, so you still need the specific grade. The table connects common filler codes with the names and applications you are likely to see on product data sheets.
Browse specialty alloy TIG rods.
| AWS classification | Familiar filler name | Common pairings and uses |
|---|---|---|
| ERNi-1 | Nickel 61-type | Commercially pure nickel, including Alloy 200/201 where this filler is specified. |
| ERNiCr-3 | Alloy 82-type | Alloys such as 600 and 601, together with selected dissimilar-metal combinations. |
| ERNiCrMo-3 | Alloy 625-type | Alloy 625 and other compatible corrosion-resistant or dissimilar joints. |
| ERNiCrMo-4 | C-276-type | Matching C-276 and other approved corrosion-resistant applications. |
| ERNiCrMo-10 | C-22 / 622-type | Corrosion-service joints requiring this matching or more highly alloyed filler. |
| ERNiCrMo-13 | Alloy 59-type | Compatible nickel-chromium-molybdenum alloys in demanding chemical service. |
| ERNiCrCoMo-1 | Alloy 617-type | High-temperature components requiring this nickel-chromium-cobalt-molybdenum composition. |
| ERNiFeCr-1 | Alloy 65-type | Alloy 825 and other compatible nickel-iron-chromium applications covered by the product guidance. |
| ERNiCu-7 | Monel 60-type | Alloy 400 and other approved nickel-copper or dissimilar joints. |
The service conditions can change an otherwise familiar pairing. For example, some Alloy 690 applications require a higher-chromium 52-type filler, so Alloy 82 should not be chosen automatically. In demanding corrosion service, a filler may also be more highly alloyed than the parent metal. These are situations where the manufacturer’s application guidance helps explain the choice made in the welding procedure.
If you are moving to nickel alloys from ordinary steel work, you may notice that the weld pool flows less readily. Good access to both joint faces makes it easier to position the arc and add filler where it is needed. Give preparation plenty of attention as well, because small amounts of contamination can contribute to cracking.
Copper and Copper-Nickel TIG Rods (AWS A5.7)
With copper-based fillers, it helps to think about the job the finished joint will do. An electrical connection may depend on conductivity, a seawater pipe on corrosion resistance, and a bronze repair on resistance to wear. Those priorities lead to different filler choices, so identifying the copper alloy is the first step towards finding a rod that provides the properties you need.
You can explore copper and bronze products in the copper and brazing filler range, with copper-nickel products also worth looking for in the specialty alloy range. Use the individual product description to distinguish the alloy and its intended welding or brazing process.
| AWS classification | Alloy type | Where it fits |
|---|---|---|
| ERCu | Deoxidised copper | Compatible copper joints and repairs. For electrical work, the deposited-metal conductivity is an important part of the product specification. |
| ERCuSi-A | Silicon bronze | Compatible copper-alloy welding and selected TIG brazing applications on steel. |
| ERCuSn-C | Tin bronze, often called phosphor bronze | Compatible bronze castings, overlays and repairs to worn surfaces. |
| ERCuNi | Nominally 70/30 copper-nickel | Commonly used for both 90/10 and 70/30 copper-nickel joints, including seawater pipework. |
| ERCuAl-A2 | Aluminium bronze | Selected copper-alloy repairs, dissimilar joints and wear-resistant overlays. |
Copper-nickel is a useful example of why the filler does not always copy the parent metal. Pipe described as 90/10 contains a different proportion of nickel from 70/30 pipe, yet a nominal 70/30 ERCuNi filler is commonly used for both. If you are considering a 90/10 filler, its suitability needs to be established from the welding procedure and corrosion requirements of the system.
The way these alloys handle heat also changes how you approach the weld. Pure copper carries heat away quickly, which can make preheat, gas choice and available power important on heavier sections. Copper-nickel carries heat away much less readily, so the same preheat treatment should not be carried over automatically. The preparation and settings need to suit the particular alloy.
TIG Brazing and Bronze Filler Rods
TIG brazing is worth understanding if you work with thin steel or certain dissimilar joints. The arc melts the filler and heats the parent metal so that the filler can spread across and bond to its surface, without deliberately melting the parent metal. That can help limit distortion, but it produces a different kind of joint from a fusion weld. The design must allow for brazing and its required strength before it is used in place of a specified weld.
Browse brazing and bronze TIG rods.
| Filler | Typical use | Understanding the application |
|---|---|---|
| ERCuSi-A — silicon bronze | TIG brazing of suitable steel joints, including some panel and repair work. | The design must allow for a brazed joint. On vehicle repairs, the manufacturer’s method determines which joining process can be used. |
| ERCuAl-A2 — aluminium bronze | Some dissimilar joints, copper-alloy repairs and overlays. | The parent metal and procedure determine whether the application is brazing or fusion welding. |
| ERCuSn-C — tin bronze | Compatible bronze repairs and surfacing. | Its bronze composition identifies a filler family; it does not establish suitability for general TIG brazing of steel. |
| ERCu — deoxidised copper | Compatible copper fusion welds and repairs. | Usually chosen for copper welding, with different applications from silicon-bronze filler. |
| CuP / Ag-CuP brazing alloys | Brazing compatible copper pipework. | A separate brazing-filler family, commonly classified under AWS A5.8. Use the product’s stated heating method rather than treating it as an ordinary TIG rod. |
On galvanised parts, lower heat can reduce damage to the zinc coating around the joint, although some coating damage and zinc fume can still occur. The preparation method and effective fume control therefore remain important parts of the work.
Copper-phosphorus rods are another product you may encounter in a brazing range, particularly for copper pipework. They can be self-fluxing on copper, but their chemistry makes them unsuitable for brazing steel or nickel alloys, where brittle compounds can form. Keep that distinction in mind when comparing them with TIG brazing products.
Cast Iron TIG Filler Rods (AWS A5.15)
Before choosing a rod for cast iron, take a close look at the casting and the repair it needs. Its shape, condition and freedom to expand and contract can be as important as the area you intend to weld. Nickel-based fillers are useful because they can leave a ductile, machinable deposit, although the cast iron beside the weld can still harden or crack. Oil-soaked castings and heavily restrained joints need particular care.
The specialty alloy TIG rod range is the place to look for bare cast-iron fillers. The product data sheet will identify the casting types and processes each one is intended for.
| Bare filler type | Where it may be useful | Choosing a suitable product |
|---|---|---|
| ERNi-CI | Cast-iron repairs needing a nickel-rich, machinable deposit. | Choose a product supplied and approved as a bare filler for the process you will use. |
| Nickel-iron or nickel-iron-manganese bare fillers | Repairs needing greater deposit strength or compatibility with ductile iron. | ERNiFeMn-CI is one bare-filler classification. Nickel-iron products differ, so composition and TIG suitability need to be established from the individual data sheet. |
When comparing products, pay attention to the prefix as well as the nickel content. ENi-CI and ENiFe-CI identify covered electrodes for MMA welding, so they are different consumables from the bare TIG fillers in this section. Removing an MMA electrode’s coating does not turn it into a correctly specified TIG rod.
A workable repair plan brings the filler, welding method and heat control together. The casting determines the approach to preheat, bead length, any peening and cooling, so a technique that suits one repair may not suit the next. It is also worth deciding at this stage whether TIG is the best process for the job; MMA, brazing or a mechanical repair may offer a more suitable route.
Hardfacing TIG Filler Rods (AWS A5.21)
For a worn component, start by separating the need to restore its shape from the need to protect its surface. Build-up replaces missing material underneath, while hardfacing provides the final wear-resistant layer, and those jobs may need different fillers. TIG is useful where you want closely controlled deposits on a small tool or detailed repair. The choice of alloy then comes down to what is causing the wear: abrasion, impact, rubbing contact, heat or a combination of them.
The hardfacing TIG rods range provides a starting point for comparing those alloy families. Individual product data sheets give the intended process, deposit properties and application guidance.
| Filler family | Common uses | What influences the choice |
|---|---|---|
| Tool-steel types | Repairs to dies, punches, blades and tooling faces. | The tool-steel grade, heat treatment and finishing method. A hardened deposit may need grinding rather than ordinary machining. |
| Chromium-carbide types | Abrasive wear from sand, soil and minerals. | The amount of impact as well as abrasion, mixing with the parent metal, and the permitted number of layers. Some grades develop relief cracks during cooling. |
| Austenitic manganese types | Components exposed to repeated impact and compressive loading. | The way the deposit hardens in use, together with temperature control when working on manganese steel. |
| Cobalt-based types | Valve seats, hot-wear surfaces and some tooling applications. | The grade’s ability to retain hardness at temperature, resist corrosion and accept the required finishing process. |
Think about how the wear occurs before choosing by hardness alone. An alloy that resists abrasion can still fail under heavy impact, while a tough build-up layer may wear too quickly if it is left as the working surface. This is why manufacturers recommend combinations of buffer, build-up and hardfacing materials for particular jobs.
Follow that system when a buffer layer is needed, rather than treating 307Si or 309L as a universal first layer. Some hardfacing deposits also develop expected relief cracks as they cool, but those cracks must be distinguished from unacceptable cracking in the parent component.
Choosing Rod Diameter and Keeping Fillers Clean
Once you have chosen the filler alloy, the next decision is the rod diameter. Think about how much metal you need to add and how easily you can feed it into the pool. A smaller rod gives you finer control over small additions, which is useful when the pool is small. A larger rod adds more metal with each movement, but needs enough heat to melt smoothly without cooling the pool too much. Sizes such as 1.0, 1.6, 2.4 and 3.2 mm are common, with availability depending on the alloy.
Material thickness gives you a starting point, then joint shape, current, welding position and your feed rate help refine the choice. On a thick joint built up in several passes, for example, you may not want the same large rod throughout. Follow the rod sizes in the welding procedure where one applies, or try the size on representative test material to see whether you can maintain a steady pool and feed the filler comfortably.
Once the rods reach the workshop, a simple storage routine helps preserve both their condition and their identity. Keep each grade dry and clean in its own labelled container, with batch details and certificates where the job requires traceability. If a rod becomes oxidised or contaminated, use the manufacturer’s cleaning guidance. Keep unidentified offcuts separate so that they cannot be mistaken for the grade marked on a tube.
Before You Order
By the time you order, you should have a clear picture of the metals being joined, the properties the weld needs and the rod size you intend to use. The TIG Rod Finder can help narrow the options, or you can compare products in the full TIG filler rod range. For work covered by a welding procedure, make the final comparison against that document and the product data sheet so the consumable you buy matches the job you have planned.